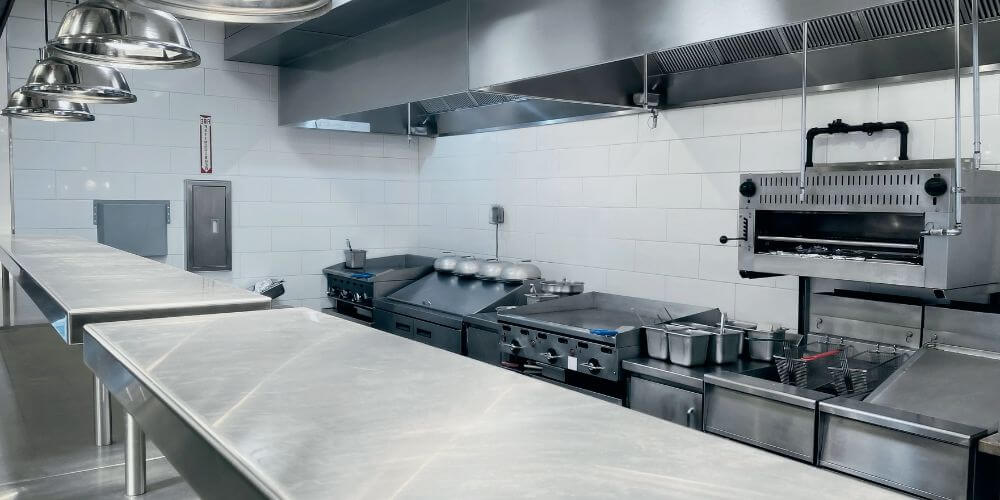
Antimicrobial technology for commercial kitchens is among the various innovations that aid the food and catering sectors, where hygiene is a priority and a non-negotiable necessity to maintain optimal hygiene standards. BioCote® antimicrobial technology inhibits the growth of bacteria such as Listeria monocytogenes, Campylobacter, and Salmonella that often pose a significant risk throughout the food supply chain.
Proven Efficacy and Key Benefits
BioCote® antimicrobial technology sets itself apart with its high proven efficacy against bacteria, with a 96% reduction in bacteria in a food production facility. Furthermore, BioCote® is the first and only antimicrobial technology globally to receive HACCP International certification, which allows us to be integrated for direct use in food-contact items. However, the benefits of antimicrobial technology extend beyond enhanced hygiene.
- Extended Product Lifespan: Antimicrobial technology not only contributes to a cleaner kitchen but also helps extend the lifespan of equipment and surfaces. By inhibiting microbial growth, it reduces the deterioration of materials, ensuring that kitchen components remain in good condition for a longer period of time.
- Reduced Cross-Contamination Risks: In a busy commercial kitchen, cross-contamination is a constant concern. Antimicrobial coatings and products create a protective barrier, minimising the risk of cross-contamination from one surface to another by preventing the spread of microbes from one surface to another.
- Ease of Maintenance: Antimicrobial surfaces are often easier to clean and maintain. They resist the accumulation of bacteria, making regular cleaning routines more effective and efficient.
Diverse Applications
Commercial kitchens need to meet strict cleanliness standards and ensure a consistently clean environment. As surfaces are often exposed to high traffic, moisture, and varied temperatures, they can become breeding grounds for bacteria and microbes.
BioCote®’s technology can provide a layer of protection to a diverse array of products; from walls and flooring to conduits and trays, these products can then seamlessly combine functionality with advanced antimicrobial protection. Antimicrobial technology can be introduced into the product itself or its surface, allowing for a tailored approach to address specific needs and challenges.
Antimicrobial Paints and Coatings for Commercial Kitchens
Paints, integrated with BioCote® antimicrobial technology, play a crucial role in enhancing safety and hygiene standards in commercial kitchens. Antimicrobial paints and coatings are particularly beneficial in spaces prone to surface-to-surface cross-contamination, especially in food preparation areas. Representing a versatile and cost-effective solution, antimicrobial paints are also seamless and hassle-free in their application.
In collaboration with Akzo Nobel with their Interpon Range, Cardinal, Powder Tech, and other leading paints and coatings partners, BioCote® offers an additional layer of protection. By applying them to surfaces such as walls, ceilings, equipment surfaces, and existing features, businesses can rely on BioCote® antimicrobial additives to actively inhibit bacterial growth. This proactive approach ensures a consistently cleaner kitchen environment and reflects a commitment to enhance hygiene standards.
Collaborative Innovation: BioCote® Partners in Food
Renowned brands in the food industry recognise the value of BioCote® antimicrobial technology in enhancing the hygiene of their products. Touchscreens and portable devices are recognised as breeding grounds for microbes; therefore, Monika focused on developing a handheld Smart PA device, ensuring functionality and cleanliness in high-use kitchen environments. Similarly, ABB introduced an antimicrobial conduit system, providing resilient protection for crucial power and data cables. CDN offers a range of thermometers that benefit from proven antimicrobial technology to ensure that its thermometers reduce the presence of microbes on their surfaces, keeping them fresher for longer and extending their functional lifetime.
In partnership with John Lord, a leader in high-performance resin flooring, advanced antimicrobial technology extends its reach to the very foundation of commercial kitchens. Simultaneously, BioClad®, an award-winning manufacturer, introduces antimicrobial wall cladding designed to combat bacteria and microbes on the very surface of walls. As businesses strive for excellence and consumers demand higher hygiene standards, BioCote® stands as a trusted partner in the pursuit of a cleaner, safer, and more resilient commercial kitchen environment.

MEBSS : Managing Microorganisms In Veterinary Environments
BioCote® conducted targeted testing against the MEBSS panel, five bacteria relevant to veterinary environments, including MRSA, E. coli, Bordetella, Salmonella, and Streptococcus. Using ISO 22196 methodology, results demonstrated up to 99.98% reduction across all organisms tested, supporting improved surface performance alongside routine cleaning practices.
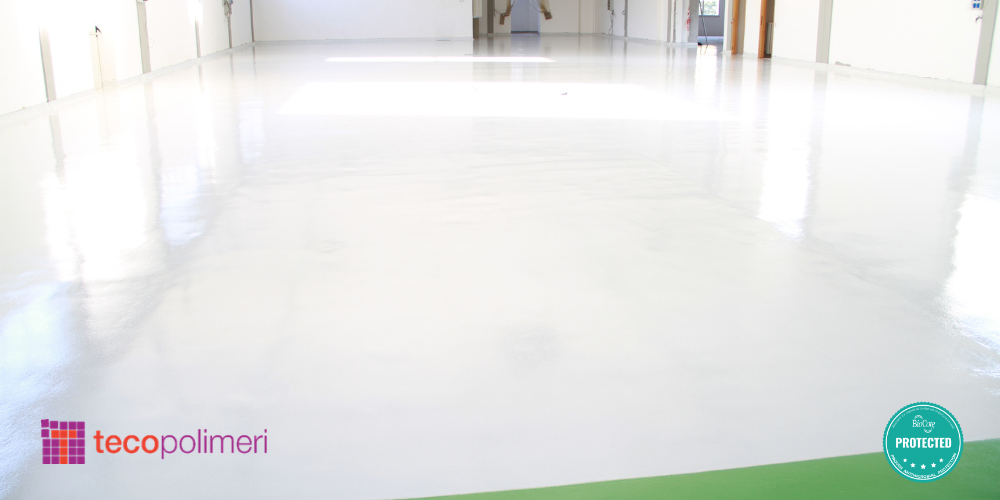
Elevating Hygiene from the Ground Up with Teco Polimeri
Italian flooring specialist Teco Polimeri has integrated BioCote® antimicrobial technology directly into its Linea Antibatterica epoxy resin systems. Designed for demanding food, pharmaceutical, and healthcare environments, these seamless, durable floors provide continuous surface protection against bacterial growth between routine cleaning cycles.